For B2B buyers, China sheet metal fabrication can be attractive because the supplier base is broad, process capability is mature, and many factories are used to export documentation, custom drawings, and recurring production. The challenge is that quotes can vary widely, even for the same part drawing.
A low price is not always a true saving. It may exclude deburring, inspection, surface treatment, protective packaging, or the fixtures needed to keep welded assemblies consistent. It may also depend on a minimum order quantity that is unrealistic for your launch plan or inventory budget.
Cost, quality, and MOQ should therefore be evaluated as one sourcing decision. A useful quotation should show, or at least clearly explain, the major cost elements: material, cutting, bending, welding, finishing, inspection, packaging, and any tooling or fixture charges. Finish selection also matters. Powder coating, plating, anodizing, brushing, and polishing can affect not only the unit price but also batch scheduling, lead time, and acceptable defect criteria.
Key Cost Drivers in China Sheet Metal Fabrication
The starting point for any sheet metal quote is the material. Carbon steel, stainless steel, aluminum, galvanized steel, copper, and brass all have different raw material prices, availability, forming behavior, and finishing requirements. Within each category, the exact grade matters. For example, stainless steel 304 and 316 are not interchangeable in cost or corrosion performance. Aluminum grades also differ in bendability and surface treatment suitability.
Sheet thickness is another baseline cost driver. Thicker material increases raw material consumption and may require more cutting power, larger bend radii, stronger press brake capacity, and additional handling time. Very thin sheet can reduce material cost but may increase quality risk, especially if the design includes large flat panels, cosmetic surfaces, or welding.
After material, the main fabrication steps add labor, machine time, and setup effort:
| Cost element | What buyers should check |
|---|---|
| Cutting | Laser cutting, punching, shearing, edge quality, nesting efficiency, pierce marks, burr control |
| Bending | Number of bends, bend sequence, tooling needs, angle tolerances, risk of interference |
| Welding | Weld length, welding method, fixture requirements, grinding, distortion control |
| Finishing | Powder coating, plating, anodizing, brushing, polishing, masking, color matching |
| Inspection | First-article inspection, dimensional checks, coating checks, material certificates |
| Packaging | Surface protection, separators, export cartons, pallets, corrosion prevention |
Fabrication is often more cost-effective than CNC machining for brackets, panels, trays, covers, cabinets, and enclosures. A part that would require removing a large amount of metal from a billet may be cheaper when cut and bent from sheet. However, this advantage depends on the design being suitable for sheet metal processes. Too many bends, tight internal corners, heavy welding, or unnecessary cosmetic requirements can quickly reduce the cost benefit.
Finishing deserves special attention because it is often priced by batch rather than by individual piece. Powder coating may require color setup, hanging fixtures, curing time, and minimum batch handling. Plating and anodizing may have minimum lot charges, surface preparation requirements, and longer scheduling windows. A small order using a non-standard finish can therefore have a high unit cost even if the metalworking itself is simple.
Buyers should compare total landed cost, not only ex-works unit price. A realistic sourcing calculation includes:
- Engineering review and drawing clarification
- Prototype or sample cost
- Tooling, jigs, or welding fixtures
- Surface treatment minimum charges
- Inspection and testing requirements
- Export packaging
- Freight, duties, and destination handling
- Buffer for rework, replacement, or schedule delay
When comparing suppliers, ask each one to quote the same drawing revision, material grade, finish specification, quantity, packing method, and delivery term. Otherwise, the lowest quote may simply reflect different assumptions.
MOQ Planning: From First Prototypes to Production Runs
Many Chinese sheet metal shops can quote single prototypes or very small batches if the drawings and specifications are complete. This is useful for product validation, fit checks, design revisions, and pre-production testing. However, buyers should expect prototype unit prices to be much higher than production prices.
The reason is simple: setup work does not disappear just because the order is small. The supplier still needs to review drawings, program laser cutting or punching equipment, select bending tools, prepare welding instructions, arrange material, and inspect the finished part. When those setup costs are spread across one or ten pieces, the unit price is naturally high.
As quantity increases, pricing usually improves at clear breaks. A supplier may quote significantly different unit prices for 20, 100, 500, and 2,000 pieces. The exact curve depends on material yield, cutting time, bending efficiency, finishing batch size, packaging, and whether fixtures are required.
MOQ can also be driven by process constraints rather than by the factory’s sales policy. For example:
- A powder coating shop may prefer a minimum batch for a custom color.
- A plating supplier may have minimum tank or lot charges.
- A welded assembly may require a fixture that only makes sense above a certain quantity.
- A material grade or thickness may have a minimum sheet purchase quantity.
- Custom packaging may have its own MOQ from the carton or foam supplier.
For early-stage sourcing, it is better to ask for several quantity levels rather than one number. A practical RFQ can request prices at, for example, 10, 50, 200, 1,000, and 5,000 pieces. This shows how the cost changes as the order grows and helps procurement plan inventory, cash flow, and launch risk.
Buyers should also clarify whether the quoted MOQ applies to the part, the finish, the color, or the total order. A factory may accept 50 pieces of a simple bent bracket but require 300 pieces for a custom powder-coated enclosure. If the product has multiple sheet metal components, ask whether the MOQ applies per component or per assembled set.
For new products, a staged approach is often safer:
- Prototype sample for fit and function.
- Small pilot run for assembly and packaging validation.
- First production order after drawings and inspection criteria are frozen.
- Larger repeat orders after field feedback and demand are confirmed.
This approach may not deliver the lowest unit cost at the beginning, but it reduces the risk of buying a large batch of parts with unresolved design or quality issues.
Controlling Quality in Bends, Welds, Holes, and Surface Finishes
Sheet metal quality problems are often process-related. The most common risks include incorrect bend angles, inconsistent flange lengths, misaligned holes, weld distortion, visible grinding marks, coating defects, scratches, and color variation. These problems can affect assembly, appearance, durability, or compliance with customer requirements.
Bending quality depends on material thickness, grain direction, bend radius, tooling, bend sequence, and operator control. If holes, slots, or cutouts are too close to bend lines, they may deform during forming. Designers can reduce defects by keeping features away from bend zones, using realistic bend radii, and avoiding unnecessarily tight tolerances on non-critical flanges.
Hole alignment is especially important for parts that assemble with screws, rivets, hinges, gaskets, rails, or electronic components. Laser-cut or punched holes on a flat blank can often be controlled more tightly than features affected by bending or welding. If a hole position is critical after forming, the drawing should define whether the tolerance applies before or after bending.
Welding adds another layer of variation. Heat input can pull parts out of position, especially on thin panels or long seams. Warping is a common risk when the welding sequence, tack weld pattern, or fixture design is not controlled. A supplier producing welded enclosures, frames, or panels should be able to explain how it controls distortion, whether through jigs, staggered welding, clamping, cooling time, or post-weld straightening.
Surface finish quality should be defined before production begins. “Black powder coating” is not enough for many B2B projects. Buyers may need to specify color standard, gloss level, texture, coating thickness, corrosion resistance expectations, masking areas, acceptable touch-up methods, and appearance criteria. For brushed or polished stainless steel, grain direction and protective film handling should be defined.
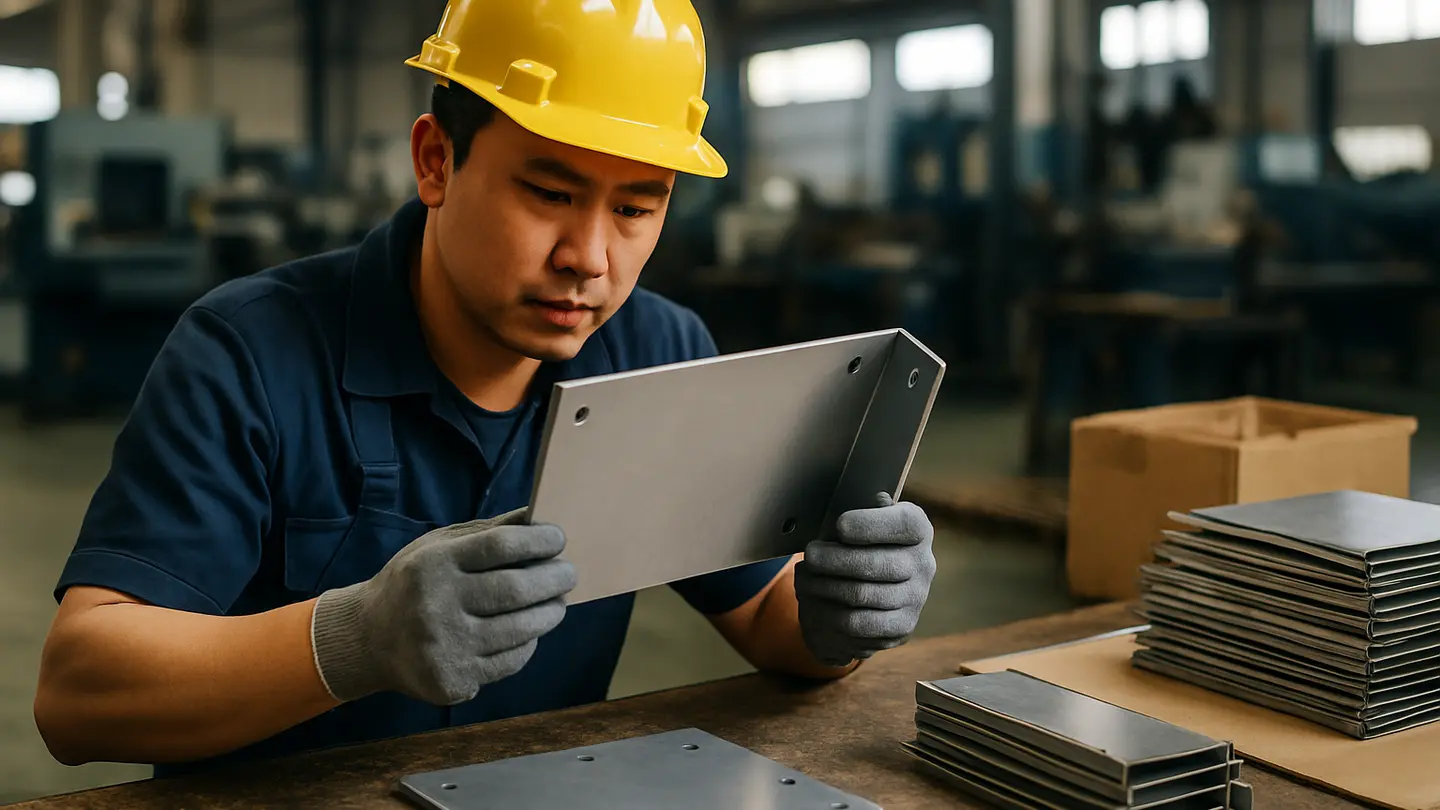
First-article approval is one of the most important controls. The first article should be produced to the latest drawing revision, using the intended material, process route, finish, and inspection method. Approval should not be based only on photographs. For critical parts, buyers should request a dimensional report, finish checks, photos of key features, and confirmation of any deviations.
Material certificates should be checked when alloy grade, corrosion performance, food contact, fire safety, electrical grounding, or regulatory compliance is important. For non-critical brackets or internal covers, full traceability may not be necessary. But for parts used in demanding environments, the wrong material grade can create serious warranty or safety risk.
A clear drawing package should include:
- 2D drawings with dimensions, tolerances, and revision number
- 3D files when geometry is complex
- Material grade and thickness
- Surface finish specification
- Critical-to-quality dimensions
- Welding symbols or assembly notes where needed
- Inspection requirements
- Packaging and handling instructions for cosmetic parts
Quality improves when the supplier knows which dimensions and surfaces matter most. Without that guidance, inspection resources may be spent on non-critical features while assembly-critical dimensions receive insufficient attention.
FAQ
Q1: Which materials and finishes can Chinese fabricators usually do?
Common materials include carbon steel, stainless steel, aluminum, and galvanized steel. Many suppliers can also process copper or brass, although availability, cutting behavior, and surface protection requirements may differ from standard steel or aluminum parts.
Typical finishes include powder coating, anodizing, electroplating, brushing, polishing, passivation, and sometimes painting or electrophoresis coating depending on the supplier network. Not every fabricator performs all finishing in-house; many use specialist subcontractors for coating, plating, or anodizing.
Buyers should confirm the material grade and finish standard in writing. If the part requires a specific alloy, coating thickness, color code, gloss level, corrosion test, or cosmetic standard, include it in the RFQ and drawing package rather than relying on general descriptions.
Q2: Will the factory suggest design changes to lower my cost?
Capable suppliers may provide design-for-manufacturing feedback, especially when they see opportunities to simplify cutting, bending, welding, finishing, or assembly. These suggestions can reduce cost and improve production consistency.
Common examples include reducing the number of bends, using a standard sheet thickness, increasing bend radii, changing hole positions away from bend lines, replacing some welded joints with folded tabs, or using pressed-in fasteners instead of complex welded hardware. In some cases, a part can be redesigned to reduce separate components or avoid an expensive fixture.
Buyers should review these suggestions carefully. A lower-cost design must still meet strength, appearance, safety, assembly, and service requirements. The best outcome is not simply the cheapest part, but the simplest design that performs reliably in production.
Q3: Should the assembly be welded or bolted together?
Welding can provide strength, rigidity, and a clean finished appearance. It is often suitable for frames, sealed structures, permanent assemblies, and products where visible fasteners are undesirable. However, welded assemblies can be harder to rework and may distort thin panels if fixturing and welding sequence are not well controlled.
Bolts, rivets, or pressed-in fasteners can make sense when the assembly needs to be repaired, replaced, adjusted, or shipped flat. Fastened designs can reduce welding distortion and may simplify coating if parts are finished separately before assembly. They can also support modular product families where different panels or brackets are combined.
The choice should balance strength, appearance, service access, finishing sequence, packaging volume, installation labor, and logistics cost. For export products, flat-pack or semi-assembled designs may reduce freight volume, but they can increase final assembly work.
Q4: How tight can tolerances be on bends and holes?
Sheet metal fabrication generally holds looser tolerances than CNC machining because bending, springback, welding, coating, and assembly all introduce variation. Flat laser-cut or punched features can often be controlled more tightly than bend angles, formed dimensions, or welded assemblies.
Cut holes, slots, and profiles may be accurate on the flat blank, but their final position can shift after bending. Bend angles may vary with material batch, thickness variation, grain direction, tooling, and operator settings. Welded assemblies introduce additional movement from heat distortion and fixture tolerance.
Buyers should mark critical dimensions clearly. If a hole pattern must align with another component, if a flange angle affects sealing, or if a cosmetic gap is important, identify it on the drawing. This allows the factory to focus process control and inspection where it matters most instead of applying unrealistic tolerances across the entire part.
Final Takeaways for Comparing Quotes and Suppliers
When sourcing China sheet metal fabrication, price, quality, and MOQ should not be reviewed separately. They are connected. A low unit price may depend on a high MOQ, a simplified finish, limited inspection, lower-grade material, or assumptions that do not match the buyer’s application.
A strong supplier should be able to explain the process route, including material sourcing, cutting, bending, welding, finishing, inspection, packaging, and any subcontracted steps. The quote should make key assumptions visible. If the supplier cannot explain how it will control bends, welds, hole alignment, and coating consistency, the buyer should treat the quote with caution.
The most useful comparison is not “which supplier is cheapest?” but “which supplier offers the best controlled total cost for the required quality level and order plan?” That means reviewing samples, first-article reports, finish standards, material certificates when needed, packaging methods, and realistic lead times.
For production success, freeze the drawing revision, define critical dimensions, approve first articles, and confirm surface finish criteria before mass production. These steps add discipline at the beginning, but they prevent expensive disputes later.