Types of Parts and Hardware to Source
Hardware sourcing from China can cover a broad range of custom and standard metal components used in shower enclosures, bathroom accessories, household products, machinery, and consumer goods. The appropriate sourcing route depends on the part geometry, annual volume, cosmetic expectations, functional loads, and target selling market.
Common categories include:
- CNC-machined parts: Suitable for precision components such as shower door hinges, connector blocks, brackets, knobs, threaded inserts, guide components, and custom fittings. CNC machining supports tight tolerances and is often practical for prototypes and lower-volume runs. Buyers should define critical dimensions, thread specifications, surface finish, and mating-part requirements.
- Laser-cut sheet-metal components: Often used for mounting plates, support brackets, cabinet panels, covers, frames, and bent sheet-metal structures. Laser cutting avoids the upfront cost of dedicated stamping tools, but cut-edge quality, burr removal, bend accuracy, and distortion after welding require attention.
- Die castings: Zinc- or aluminum-alloy die castings can be appropriate for complex-shaped hardware produced in higher quantities. Common concerns include porosity, dimensional stability, wall thickness, strength at load-bearing points, and finish suitability for plating or coating.
- Stampings: Metal stampings can be economical once quantities are high enough to justify tooling. They are commonly used for repetitive flat or formed components. Tool design, burr direction, springback, and consistency across long production runs should be considered during development.
- Finished hardware: This category may include handles, hinges, rollers, fasteners, brackets, clamps, towel hooks, and decorative fittings. For bathroom-related hardware, corrosion resistance, smooth edges, surface uniformity, and moving performance are often as important as basic dimensions.
Material choice affects both performance and manufacturing cost. Aluminum may suit lightweight machined or extruded components. Stainless steel is widely considered where corrosion resistance is important. Carbon steel may be appropriate for coated structural parts, while brass and zinc alloys are often used for decorative or die-cast hardware. The required material grade should be stated before final quotation and production approval.
Process-specific risks should be discussed early. A CNC part may meet dimensions but have an unsuitable cosmetic machining finish. A laser-cut part may have sharp edges or heat-related distortion. A die casting may look acceptable externally while containing internal porosity that affects strength or finishing. A stamped part may have inconsistent bends if the tool or material condition is not adequately controlled.
Compliance requirements also depend on the end product and destination market. A hardware component intended for a shower enclosure, for example, may need to satisfy the buyer’s internal corrosion, load, or durability requirements, while a component used in another product category may be subject to different functional or material expectations. The supplier should not be asked to infer these requirements from product photos alone; they should be written into the technical package wherever possible.
Prototype quantities can be very low, particularly for CNC machining or laser cutting. Production minimums often rise when dedicated tooling, casting dies, automated finishing, branded packaging, or customized cartons are needed. Buyers should therefore distinguish between the quantity needed to validate a design and the quantity required for an economical production program.
Moving from a Drawing to Repeatable Production
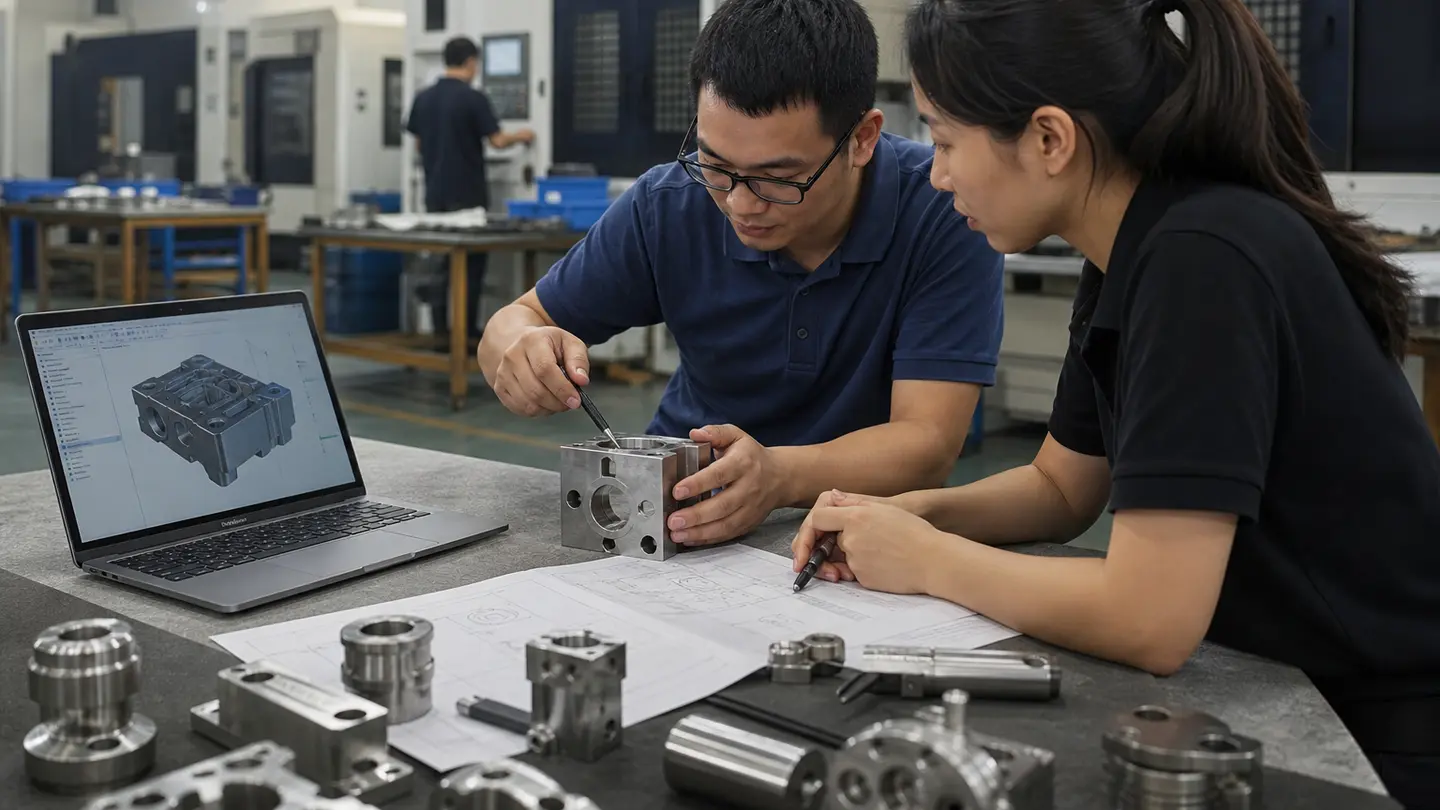
Successful hardware sourcing from China starts with a technical package that gives suppliers a consistent basis for quotation and manufacturing. For custom parts, the most useful package usually combines a 3D CAD model, a dimensioned PDF drawing, material requirements, finish requirements, and information about the part’s intended function.
STEP and IGES files are useful because they allow suppliers to review geometry, estimate machining time, identify difficult features, and plan manufacturing operations. However, a 3D model alone may not communicate every requirement. The PDF drawing should identify critical dimensions, tolerances, threads, materials, surface treatments, cosmetic surfaces, and any special inspection points.
Physical samples can also help, especially when replacing an existing component or developing a part without complete engineering documentation. A sample may be measured and converted into a working drawing, but the resulting drawing should be reviewed and approved by the buyer. Once approved, it becomes the inspection reference rather than the original sample alone.
The first article is the key transition point between development and production. Before authorizing a batch, buyers should compare the first article against the approved drawing and intended assembly. This review should include critical dimensions, fit with mating parts, material confirmation, finish quality, and function. For moving shower hardware, that may include hinge movement, roller travel, screw engagement, alignment, and the part’s interaction with glass, seals, rails, or brackets.
A prototype process is not always the best production process. CNC machining is often useful for validating a design before investing in casting or stamping tooling. It can produce low quantities with relatively limited setup requirements and can reveal issues such as inaccessible tool paths, weak wall sections, thread interference, or unsuitable tolerances.
Once volumes increase, a buyer may consider moving from machining to die casting, stamping, forging, or another process. That transition should not be treated as a simple material-for-material replacement. A casting may require draft angles, different wall thicknesses, radii, and revised tolerances. A stamped part may need geometry changes to account for bend radii and springback. The production design should be reviewed before tooling is ordered.
For lower-volume sheet-metal components, laser cutting and bending can be a practical alternative to dedicated stamping tools. This is especially relevant when a product contains many unique brackets, panels, or structural pieces. It allows design changes without remaking a stamping mold, although unit cost may remain higher than a mature high-volume stamping program.
Repeatable production also depends on process control after the first article is approved. Buyers should clarify whether the supplier will retain inspection records, control material substitutions, manage revision changes, and notify the buyer before changing a manufacturing method, coating supplier, or component source. An unapproved substitution may appear minor but can affect corrosion resistance, fit, strength, or final appearance.
Practical Tools for Building a China Supplier Shortlist
Early supplier research should separate discovery from final qualification. A B2B platform such as Made-in-China.com can help buyers identify potential manufacturers and trading partners before moving into drawing reviews, sample development, factory checks, or commercial negotiation.
Its Supplier Discovery tools can be used to narrow a broad supplier search by product category and sourcing focus. For custom hardware, buyers can use this stage to compare suppliers that list relevant capabilities, such as machining, sheet-metal fabrication, die casting, finishing, or assembly.
Made-in-China.com also provides Audited Supplier listings and available Audit Reports for buyer review. According to the platform, these reports may include structured information on areas such as general company information, export trade, manufacturing capacity, quality control, and research and development capability. This information can support an initial screening process, but it should not replace drawing-specific technical review, sample approval, or independent due diligence where needed.
For a project requiring several quotations, Easy Sourcing allows buyers to submit one sourcing request, receive quotations from matched suppliers, compare responses, and request samples. A useful request should include drawings, material grades, target quantities, finish requirements, quality expectations, and destination market information so quotations are comparable.
Pre-Shipment Checks for Custom Metal Hardware
Pre-shipment inspection should be based on the approved drawing, approved sample, and confirmed production requirements. Visual inspection alone is rarely enough for custom metal hardware because some of the most important failures involve dimensions, material, thread quality, or assembly performance.
A practical inspection plan should focus first on critical dimensions. These may include hole locations, thread sizes, center distances, mating surfaces, wall thicknesses, bend angles, shaft diameters, and clearance dimensions. Sampled units should be measured against the approved drawing using methods appropriate to the tolerance and part geometry.
Material-grade confirmation is also important. The suitable evidence may include material documentation, supplier traceability records, or testing methods agreed for the project. This matters when parts are specified in stainless steel, brass, aluminum, carbon steel, or a particular alloy grade. A visually similar substitute may perform differently in corrosion exposure, machining, plating, welding, or load-bearing use.
For coated, plated, or painted parts, checks should address:
- Coverage on visible and concealed areas
- Color and appearance consistency where appearance is important
- Adhesion of the finish
- Surface defects, scratches, pits, and exposed base material
- Corrosion resistance requirements where applicable
Bathroom and shower hardware requires particular attention to finish quality because components may operate in humid environments and remain visible to end users. A coating may look satisfactory on a flat display surface but fail at edges, corners, threads, welds, or recessed zones if preparation and coverage are inconsistent.
Functional checks should reflect how the hardware will be used. Depending on the part, this may include thread engagement, screw insertion, assembly fit, hinge movement, sliding motion, locking action, load performance, or repeated movement. If a part interfaces with glass, rails, seals, or other purchased components, it should be checked in a representative assembly rather than evaluated in isolation only.
Packaging should also be inspected. Metal components can dent, scratch, chip, or puncture weak packaging during handling and ocean or road transit. Heavy parts may damage cartons if inner supports are inadequate. Packaging should protect finished surfaces, separate parts that can rub together, and provide sufficient carton strength for the packed weight.
Case Study: Vext’s 400 Smart Gardens Without Stamping Molds
A reported project for 400 indoor smart-garden cabinets illustrates why the manufacturing method should match the initial production volume. The cabinets were made largely from welded, powder-coated mild steel and contained numerous individual sheet-metal parts.
At this quantity, dedicated stamping tooling for every unique metal component was not considered economical. Stamping can be efficient for repeated high-volume parts, but a product with many different panels, brackets, and formed pieces may require multiple tools. The tooling investment can be difficult to justify before demand and product design are fully proven.
Laser cutting provided an alternative route. Sheet-metal parts could be cut without dedicated stamping molds, then bent, welded, finished, and assembled into the cabinet structure. This approach supported production while reducing the commitment to tool-specific manufacturing during the initial run.
Laser-cut edges required management. Sharp edges can create safety, handling, and assembly concerns, especially on products with multiple exposed metal panels. The project reportedly addressed this through part orientation, welding placement, inspection, and rework where necessary. In practice, buyers should specify which edges must be deburred, folded, covered, welded, or otherwise protected rather than relying on a general expectation of “smooth edges.”
The project also reportedly included full-unit functional and appearance checks before shipment to Europe. This is a useful reminder that an inspection plan should reflect the finished product, not just individual components. A cabinet may have acceptable separate panels but still show alignment problems, poor door movement, uneven coating appearance, or visible weld defects after final assembly.
For shower manufacturers and other hardware buyers, the same principle applies: use the initial order volume to select a practical process, but define the quality requirements needed for later production scale-up.
FAQ
Q1. Can you make a prototype from a sample, without drawings?
Often, yes. A physical sample can usually be measured and converted into a working technical drawing or CAD model for quotation and prototype development. The process may include measuring dimensions, identifying materials where possible, reviewing threads and interfaces, and documenting visible finish requirements.
However, a sample does not always reveal every functional requirement. Complex internal features, hidden assemblies, specific load requirements, or intended movement may require clarification from the buyer. A copied dimension may not be sufficient if the original part was designed to work within a larger assembly.
Before prototype production, the buyer should approve the resulting drawing. That approved drawing should then become the reference for prototype inspection and future revisions.
Q2. What files do you need for a quote?
STEP or IGES files are useful for manufacturing quotations because they allow suppliers to review the 3D geometry. A dimensioned PDF drawing should accompany the model wherever possible.
The drawing should identify material, critical tolerances, threads, finish requirements, key dimensions, and any cosmetic or functional priorities. If the part is part of an assembly, photos, mating-part drawings, or a physical sample can help explain fit and intended use.
Sketches and samples can support early discussions when the design is still being developed. However, a final production quotation should be based on a controlled drawing revision to reduce misunderstanding.
Q3. What materials can you make parts in?
Common materials for custom hardware include aluminum, stainless steel, carbon steel, brass, zinc alloys, and engineering plastics. The best choice depends on the part’s required strength, corrosion resistance, finish, weight, manufacturing process, and cost target.
For example, stainless steel may be selected for corrosion-sensitive bathroom hardware, while zinc alloy may suit certain die-cast decorative components. Carbon steel can be practical for structural parts when an appropriate coating is applied.
Availability and pricing may vary for uncommon grades, special tempers, or nonstandard material forms. Buyers should confirm the required grade before final quotation and again before production approval.
Q4. How long does a machined prototype take?
Prototype timing depends on part complexity, material availability, quantity, machining operations, and required surface treatment. A simple CNC-machined part made from readily available material may move faster than a part requiring multiple setups, difficult internal features, special threads, polishing, plating, anodizing, or coating.
Additional time may also be needed for drawing clarification, first-article measurement, sample shipping, and design revisions. If the prototype will later be converted to casting or stamping, the buyer should allow time for design-for-manufacturing review before tool investment.
The most reliable approach is to confirm the manufacturing and finishing timeline for the specific part before committing to a development schedule.