Choosing the right manufacturing process in China should start with the part, not with the supplier’s preferred equipment. A shower trim plate, plastic cartridge housing, zinc handle, stainless bracket, and aluminum enclosure may all come from Chinese factories, but they do not belong in the same production route.
The best process depends on four practical variables: geometry, production volume, tolerance requirements, and surface finish. Injection molding, 3D printing, die casting, CNC machining, sheet metal fabrication, and laser cutting all have valid uses, but each fits a different technical and commercial situation.
A common sourcing mistake is to request quotes before the part is fully defined. If the drawing lacks tolerances, material grade, finish standard, or expected order volume, suppliers may quote different assumptions. One factory may price a machined version, another may quote a molded or cast version, and a third may simplify features without explaining the change. The result is not a fair comparison.
For B2B buyers, process selection is both an engineering decision and a sourcing decision. The goal is not only the lowest quoted unit price, but a route that can produce the part repeatedly, economically, and at the required quality level.
How to Make the Process Decision
Before comparing factories, buyers should answer four questions:
What shape does the part have? Is it a flat panel, thin-walled housing, complex three-dimensional form, turned metal fitting, or part with undercuts and internal features?
How many units are needed? A prototype, 500-piece trial, and 100,000-piece annual program may require different processes even if the part looks similar.
How accurate must it be? Decorative parts may allow minor variation, while sealing surfaces, threaded connections, cartridge interfaces, and alignment features often need tighter control.
What appearance or finish is required? Polishing, plating, anodizing, powder coating, brushing, painting, and texture can all influence process choice.
The economic trade-off is usually between tooling-based methods and flexible production methods.
Tooling-based methods, such as injection molding and die casting, require upfront investment in molds or dies. Once the tool is running properly, unit cost can fall sharply at higher volumes. These methods suit stable designs and repeat demand.
Flexible methods, such as CNC machining, 3D printing, laser cutting, and some sheet metal operations, may avoid expensive production molds. However, they still involve setup, programming, fixtures, labor, and machine time. They are useful for early-stage work, but can become costly in large quantities.
The crossover point depends on:
- Tooling cost
- Expected lifetime demand
- Material cost
- Cycle time
- Labor content
- Scrap rate
- Future design-change risk
- Required inspection level
- Cost of delayed launch or rework
A buyer may machine a brass or plastic prototype to confirm fit, then redesign the same part for molding, casting, forging, or another scalable method once demand is predictable.
It is also important to separate mandatory requirements from preferences. Unnecessary tight tolerances or cosmetic finishes can push a part into a more expensive process. Overengineering often begins with unclear specifications.
Selecting a Process for Plastic Components
For plastic parts, the main decision usually comes down to production volume and design stability. Housings, inserts, caps, clips, handles, trays, and internal supports can often be produced by several methods, but not all methods make sense at every stage.
Injection molding is one of the most common choices for stable, higher-volume plastic parts. It is suitable when the geometry can be molded, the material is selected, and the expected order quantity can justify the mold investment. Once the mold is built and qualified, injection molding can produce consistent parts at relatively low unit cost.
Many plastic components in bathroom and shower products are molded after the design is finalized. Examples include cartridge-related parts, decorative caps, packaging inserts, mounting clips, diverter components, and internal housings. If annual demand is strong and the design is unlikely to change, tooling cost can be spread across repeat production.
However, injection molding is less forgiving when the product is still evolving. Changes to wall thickness, ribs, bosses, clips, undercuts, or parting lines can affect tooling. Buyers should avoid committing to production molds too early.
3D printing is useful for prototypes, design validation, short runs, and projects where changes are expected. It allows teams to check size, assembly, ergonomics, and general appearance before committing to tooling. Printed parts may not match final production material or finish exactly, but they can reveal design issues quickly.
For example, a buyer developing a shower control knob may print several shape variations before confirming the final geometry. A bracket can be printed to check installation clearance, or a housing can be printed to test whether internal features align with other components.
3D printing also supports low-volume projects where tooling would be uneconomical. Buyers should still be realistic about strength, finish, dimensional accuracy, and repeatability. A printed prototype is not proof that the same design can be molded without changes.
In many projects, the practical sequence is:
- 3D print early concepts
- Machine or print functional samples
- Adjust geometry for manufacturability
- Confirm resin and performance requirements
- Build prototype or production tooling
- Run first-article inspection
- Move into batch production
Avoiding tooling is valuable when uncertainty is high. Tooling becomes more attractive when both design and demand are confirmed.
Choosing a Method for Metal Parts
Metal components require a wider process review because material grade, geometry, surface finish, strength, and corrosion resistance all matter. In shower and sanitary hardware, common metal parts include handles, escutcheons, brackets, valve-related components, panels, support frames, fasteners, and decorative covers.
Die casting is often used for complex aluminum or zinc parts when expected volume justifies tooling. It can produce detailed shapes with good repeatability and is widely used for formed surfaces, bosses, ribs, and decorative geometry. Zinc die casting is common for smaller decorative or functional hardware, while aluminum die casting may be used where weight, strength, or heat resistance is relevant.
The main limitations are tooling cost and change risk. Die-cast parts need proper draft angles, wall thickness control, parting-line planning, ejector considerations, and allowance for secondary operations. Surfaces may also require polishing, plating, powder coating, or painting. Buyers should review the full route from die casting to finishing and inspection.
CNC machining is suitable for tighter tolerances, clean surfaces, prototypes, and low-to-mid production volumes. It is often used for precise interfaces, threads, flatness requirements, sealing areas, or small production batches. CNC machining can also refine castings, forgings, or extrusions by adding accurate holes, threads, grooves, or mating surfaces.
Machining is flexible because it does not require a dedicated production mold, but machine time is expensive. Complex geometry, deep cavities, tight tolerances, and high cosmetic demands can increase cost quickly. If every unit requires long machining time, buyers should ask whether casting, extrusion, stamping, or forming can create the basic shape, with only critical surfaces machined afterward.
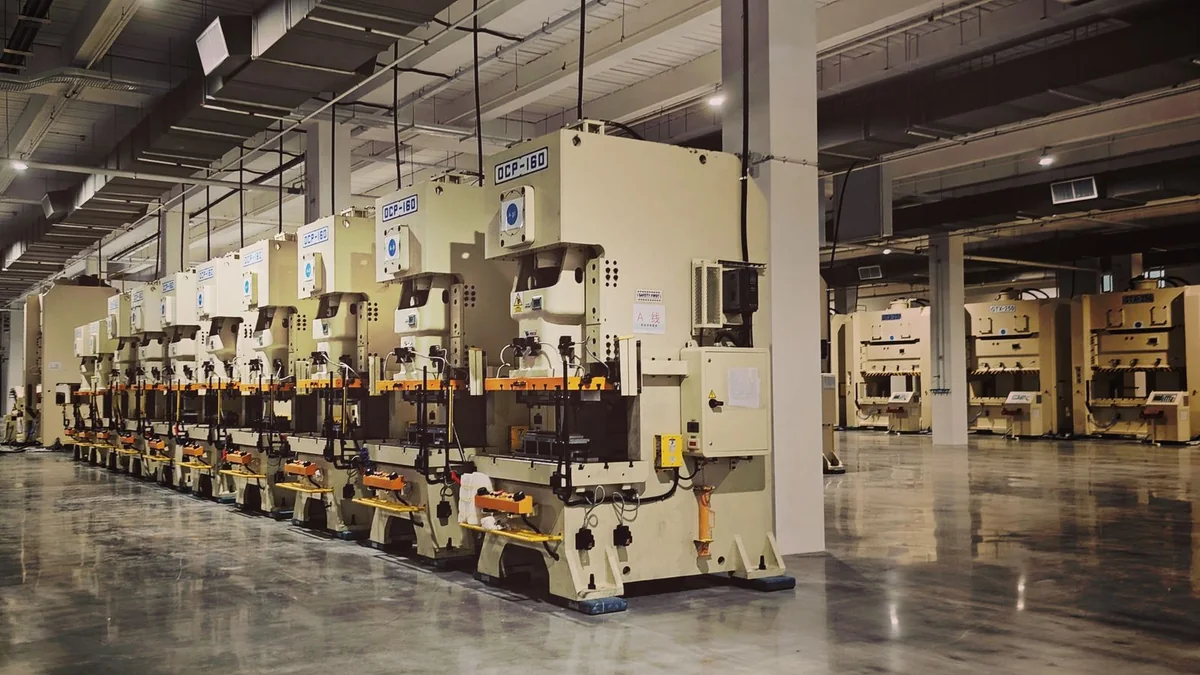
Sheet metal fabrication is efficient for brackets, panels, trays, covers, formed enclosures, and support parts. The route may include cutting, punching, bending, welding, riveting, grinding, and surface treatment. Stainless steel, galvanized steel, aluminum, and other sheet materials may be selected depending on strength, corrosion resistance, appearance, and cost.
Sheet metal is practical when the part can be developed from flat stock and then bent or formed. It is less suitable for thick, highly three-dimensional shapes with deep cavities, complex curves, or heavy machining.
Laser cutting is efficient for flat blanks, profiles, slots, and cutouts. It is useful for small and medium batches because it avoids dedicated blanking dies. However, laser cutting is rarely the whole process. Parts may still require bending, welding, tapping, deburring, brushing, coating, passivation, or assembly.
For metal parts, evaluate the complete route:
- Base material
- Cutting, casting, machining, or forming process
- Secondary operations
- Surface treatment
- Dimensional inspection
- Cosmetic inspection
- Packaging method to prevent scratches or corrosion
A low casting or cutting price can become expensive if finishing, machining, and rework are underestimated.
Moving from Prototype to Production
The right process can change as the product moves from concept to mass production. Early development usually values speed, flexibility, and low-cost iteration more than the lowest possible unit price.
At the concept stage, the buyer may not yet know whether wall thickness is correct, whether assembly is easy, or whether a decorative surface matches the desired look. In this phase, 3D printing and CNC machining help confirm fit, dimensions, user experience, and assembly logic before expensive tooling is purchased.
For shower products, this may include testing how a handle feels, whether a bracket aligns with a wall-mounting system, whether a housing clears internal components, or whether a decorative plate covers the installation area properly. Finding these issues during prototyping is far cheaper than finding them after molds, dies, or fixtures have been made.
After prototypes are approved, buyers should consider a pilot run before full-scale production. A pilot run is a controlled production test that helps reveal:
- Process variation
- Supplier capability limits
- Material handling issues
- Assembly problems
- Finish inconsistency
- Packaging damage
- Inspection workload
- Yield and scrap levels
- Lead-time assumptions
Pilot production is especially useful when a part has tight tolerances, visible cosmetic surfaces, sealing functions, or multiple secondary processes. It gives the buyer and supplier a chance to adjust work instructions, inspection plans, fixtures, packaging, and process controls before volume production begins.
Tooling-based production is safer once the design is frozen and projected demand supports the investment. “Frozen” should mean controlled drawings, material specifications, finish requirements, tolerance standards, packaging requirements, and agreed inspection criteria.
Buyers should also document what happens if design changes are needed later. Who pays for tool modification? How will old stock be handled? Does the supplier keep tool maintenance records? Are replacement cavities or inserts possible? These questions matter when the product is expected to run for years.
What to Check After Selecting the Process
Selecting the manufacturing process is only one part of successful sourcing. The supplier, material, tooling, and production controls must also match the project.
Review the selected production method together with the material grade and finish requirement. A supplier may be experienced in machining aluminum but not stainless steel. Another may be strong in plastic molding but unfamiliar with a resin that requires specific drying conditions. A die caster may produce good raw castings but rely on outside vendors for polishing or plating, adding schedule and quality risk.
Important supplier verification points include:
- Relevant equipment for the selected process
- Experience with similar materials and part types
- Inspection equipment such as calipers, gauges, hardness testers, surface roughness tools, or CMMs where needed
- Documented quality procedures
- Incoming material inspection
- In-process quality checks
- Final inspection records
- Calibration control for measuring equipment
- Clear work instructions
- Traceability for batches, materials, and finishes
- Ability to provide first-article inspection reports
Buyers should ask for evidence, not only claims. Sample parts, inspection reports, process photos, material certificates, and production records can help confirm whether the supplier understands the requirements.
Quality control should be planned before production is completed, not after finished goods are packed. Depending on the part, the plan may include:
- Material verification
- Dimensional inspection
- Functional testing
- Assembly checks
- Coating thickness checks
- Adhesion testing
- Salt spray or corrosion testing where relevant
- Cosmetic inspection under agreed lighting conditions
- Packaging drop or handling checks
- Pre-shipment inspection
Compliance should also be considered early. Shower-related products may be subject to market-specific requirements for materials, water contact, corrosion resistance, labeling, packaging, or restricted substances. Even when the supplier can produce the part, the buyer remains responsible for destination-market suitability.
Packaging, export handling, and shipping are part of the manufacturing decision. A polished or plated part can be made correctly and still arrive damaged if packaging is poor. Heavy metal components may need separators, protective film, foam, desiccants, reinforced cartons, or palletization. Plastic cosmetic parts may need scratch prevention and heat-resistant packaging.
Finally, confirm whether the supplier controls all key steps in-house or outsources some operations. Outsourcing is common, but it must be managed. If casting, machining, polishing, plating, and assembly happen at different facilities, the buyer needs clarity on responsibility, inspection points, and corrective action.
FAQ
Q1: Can a part be redesigned into a cheaper process?
Yes. Redesign can move a part into a more economical manufacturing route. Geometry changes often have a larger cost impact than material changes.
Simplifying deep pockets can reduce machining time. Adding draft angles may make molding or casting more practical. Converting a thick machined bracket into a formed sheet metal part may reduce material waste and cycle time. The key is to review manufacturability before the design is locked.
Q2: What matters more, volume or design?
Shape and material usually narrow the feasible processes first. A flat stainless panel, molded plastic clip, and complex zinc handle each point toward different methods.
After that, order quantity determines whether tooling investment is justified. Unstable designs favor flexible methods such as machining, printing, or laser cutting. Stable repeat demand makes molding, casting, or dedicated forming tools more attractive.
Q3: Do finishing and coating steps affect the choice?
Yes. Painting, plating, anodizing, polishing, brushing, powder coating, and passivation can change both cost and lead time. A base part that looks inexpensive in raw form may become costly once the required finish is included.
Define finish standards before requesting quotes. Suppliers should know the required color, gloss, texture, coating thickness, corrosion resistance, cosmetic acceptance criteria, and packaging method. Otherwise, quotes may not be comparable.
Q4: What if my part needs more than one process?
Many parts require combined processes. A die-cast handle may need machining, polishing, plating, and assembly. A laser-cut panel may need bending, welding, brushing, and protective packaging. A molded plastic part may need inserts, printing, or ultrasonic welding.
Evaluate the full manufacturing route, not only the cheapest single operation. Extra handoffs can increase rework, lead time, and quality risk. Fewer outsourced steps may simplify communication, inspection, and delivery management.
Conclusion: Match the Process to the Part and the Order
The right manufacturing process in China becomes clearer after the buyer defines shape, volume, tolerance, and finish requirements. Process choice should follow the part and order size, not simply the equipment a supplier prefers to sell.
Injection molding and die casting can be strong choices when the design is stable and volume supports tooling. 3D printing, CNC machining, sheet metal fabrication, and laser cutting can be better for prototypes, lower volumes, tighter features, or flexible development.
Successful sourcing also depends on controlled drawings, suitable material selection, supplier capability, process controls, packaging, and first-article checks. When these elements are reviewed together, buyers are more likely to achieve consistent quality, realistic pricing, and a smoother transition from sample approval to production.